OVERVIEW
Sheet-metal tooling with the edge held true.
Progressive, transfer and compound dies for trimming and forming.
±0.05 mm
Typical tolerance
0.3–6 mm
Material thickness
4–8 wk
Tooling lead time
25–800 T
Press range
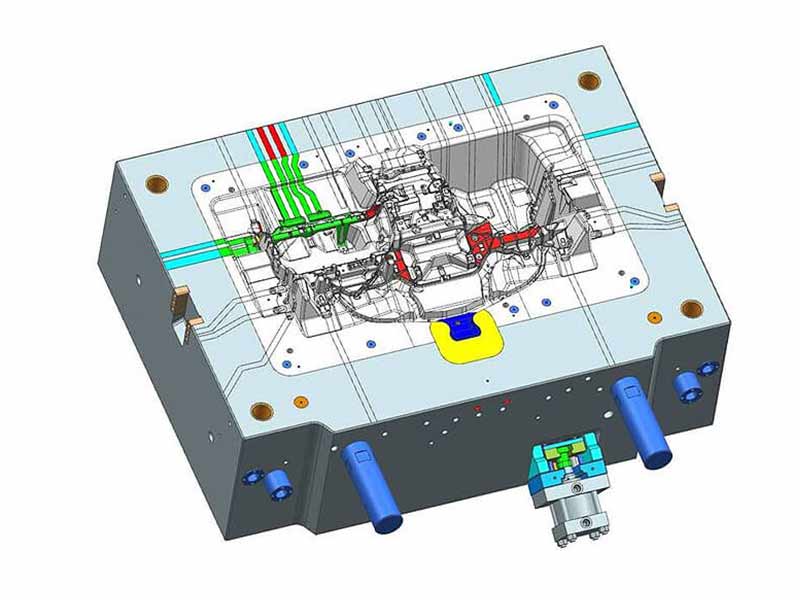
Trim dies decide the fit, edge quality and dimensional consistency of every stamped part. We design and build them around the press, the material and the production volume.
We manufacture progressive dies, transfer dies and compound dies for blanking, piercing, bending, flanging and trimming. Materials include Cr12MoV, DC53, SKD11 and SKH51, with heat treatment, surface coating and stress relief matched to the material thickness and stroke rate.
Typical parts include automotive brackets and structural components, appliance panels, electrical enclosures and hardware. We provide die design, tryout, sample inspection and spare punch/insert sets.
✓ Strip layout and material utilization
✓ Progressive, transfer and compound designs
✓ Hardened punches and replaceable inserts
✓ Tryout, samples and spare parts
CAPABILITIES
What we deliver
Practical capabilities, matched to the tooling and the production volume — not a generic menu.
01
Progressive dies
Multi-station blanking, piercing, forming and trimming with optimized strip layout.
02
Transfer dies
Robotic or manual transfer tooling for larger parts and lower volumes.
03
Blanking & piercing
Punches, dies and strippers designed for clean edges and long sharpening intervals.
04
Bending & forming
Springback control, radius consistency and forming stations matched to the part.
05
Trim & flange
Edge trimming, flanging and cam trimming for complex outer profiles.
06
Tryout & optimization
Press tryout, sample measurement, timing and strip-feed optimization.
SPECIFICATIONS
Typical range and tolerances.
Every project is quoted against the part, material and inspection requirement. Values below are typical starting points — we confirm the exact capability for your drawing.
Die type
Progressive, transfer, compound
Material thickness
0.3–6 mm
Tolerance
±0.05 mm (part-dependent)
Die life
500,000–3,000,000 strokes
Press range
25–800 T
Surface treatment
TiN, PVD, hard chrome
MATERIALS & TOOLING
Materials we work with
CR12MOV · DC53 · SKD11 · SKH51 · 45# · SKD61
Documentation
✓ Material certificates on request
✓ Dimensional report with critical dimensions
✓ Trial report and process parameters
✓ 2D drawings and spare-part list
PROCESS
How the project runs
A named project manager, weekly reporting and documented sign-off at each stage.
01
Strip & process review
Part review, strip layout, material utilization and press selection.
02
Die design
3D die design, punch and die layout, spring and cam design.
03
Build
Machining, heat treatment, grinding, EDM and assembly.
04
Tryout & handover
Press tryout, sample inspection, spare parts and documentation.
GALLERY
From the floor
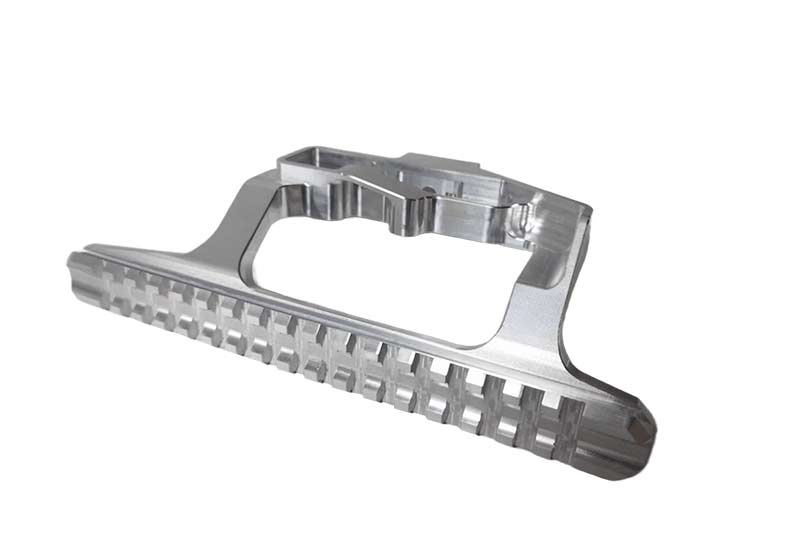
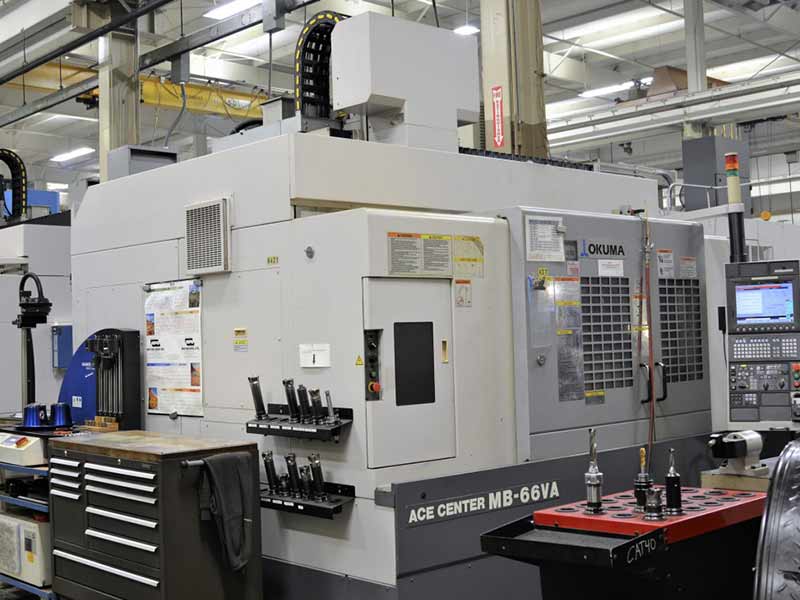
Representative tooling, machining and inspection work from our Kunshan facility.
FAQ
Questions, answered.
What material thicknesses can you tool for?
Typically 0.3–6 mm carbon steel, stainless steel, aluminum and galvanized sheet. Thicker or high-strength materials are reviewed case by case.
Do you design the strip layout?
Yes. Strip layout, material utilization, station sequence and press tonnage are part of the die design package.
Can you match an existing die?
Yes. We can reverse-engineer the part and die, or build a replacement die to the original drawings and samples.
What spare parts do you recommend?
We recommend a set of punches, die inserts and springs — typically 10–20% of the active tooling — so production is not stopped by a single wear part.
START A PROJECT
Have a mould project in mind?
Send us your part data and requirements. We will reply with a DFM review and a clear quotation within 24 hours.