OVERVIEW
Dies that hold up to heat, pressure and production.
HPDC tooling for structural, cosmetic and high-volume castings.
1–8
Cavities
±0.02 mm
Typical tolerance
6–10 wk
Tooling lead time
100k–1M
Shots
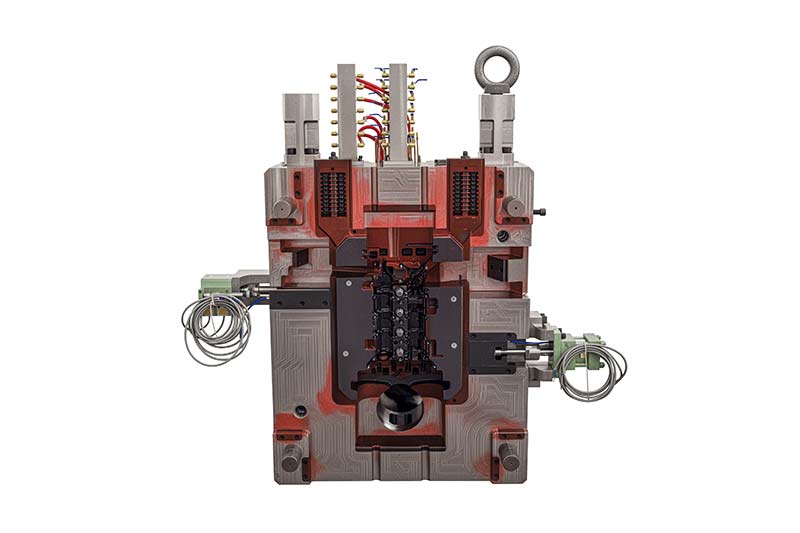
Die casting punishes tooling. Our dies are designed around thermal balance, shot pressure and cycle time — not just the cavity geometry.
We engineer high-pressure dies with single or multiple cavities, hydraulic slides, vacuum-assisted filling, jet cooling and die-spotting access. H13, SKD61 and 8407 steels are heat-treated and stress-relieved for long shot life, with inserts and cores replaceable without scrapping the base.
Typical parts include automotive housings and brackets, LED and electronics bodies, power-tool components, locks and hardware. We support die design, trial, sample inspection and trim tooling as a single package.
✓ Filling, solidification and thermal simulation
✓ Vacuum and jet-cooling options
✓ Replaceable inserts and cores
✓ Die spotting, trial and sample reports
CAPABILITIES
What we deliver
Practical capabilities, matched to the tooling and the production volume — not a generic menu.
01
HPDC die design
Runner, gate, overflow and cooling layout optimized for filling and solidification.
02
Slides & cores
Hydraulic and mechanical slides for undercuts, holes and complex side features.
03
Vacuum-assisted casting
Vacuum valve and sealing design for low-porosity structural and leak-tight parts.
04
Thermal management
Jet cooling, baffles, thermal pins and die-temperature control for stable cycles.
05
Trim dies & fixtures
Matched trim tooling, checking fixtures and secondary-operation support.
06
Tryout & optimization
Die spotting, trial shots, porosity checks and process window development.
SPECIFICATIONS
Typical range and tolerances.
Every project is quoted against the part, material and inspection requirement. Values below are typical starting points — we confirm the exact capability for your drawing.
Die type
HPDC, vacuum-assisted, squeeze casting
Cavitation
1–8 cavities (typical)
Casting size
Up to 1,200 × 800 mm
Tolerance
±0.02 mm (casting-dependent)
Die steel
H13, SKD61, 8407, 1.2344
Press range
160–2,000 T
MATERIALS & TOOLING
Materials we work with
ADC12 · A380 · A356 · AlSi9Cu3 · Zamak 3 · Zamak 5 · AZ91D · AM60
Documentation
✓ Material certificates on request
✓ Dimensional report with critical dimensions
✓ Trial report and process parameters
✓ 2D drawings and spare-part list
PROCESS
How the project runs
A named project manager, weekly reporting and documented sign-off at each stage.
01
Part & process review
DFM, draft, wall thickness, porosity risk and press selection.
02
Die design
3D die design, runner and cooling simulation, steel and slide layout.
03
Build & spot
Machining, heat treatment, EDM, assembly and die spotting.
04
Trial & validation
Trial shots, X-ray/porosity checks, dimensional report and optimization.
GALLERY
From the floor
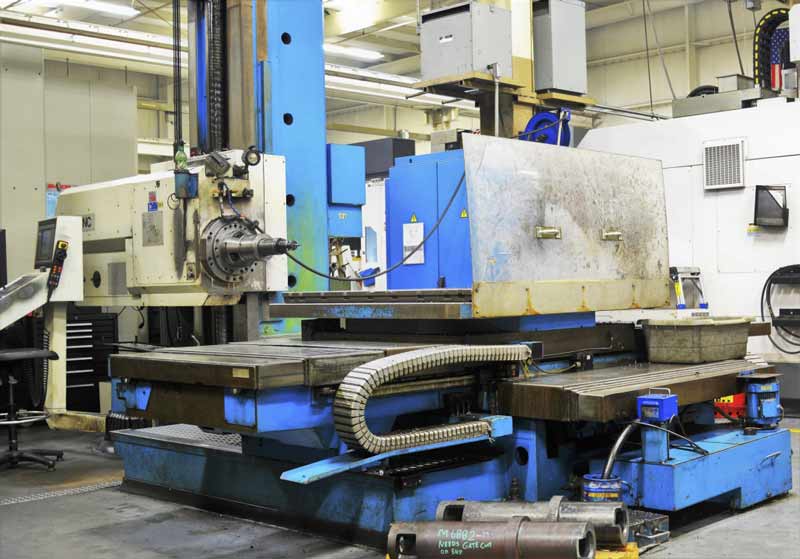
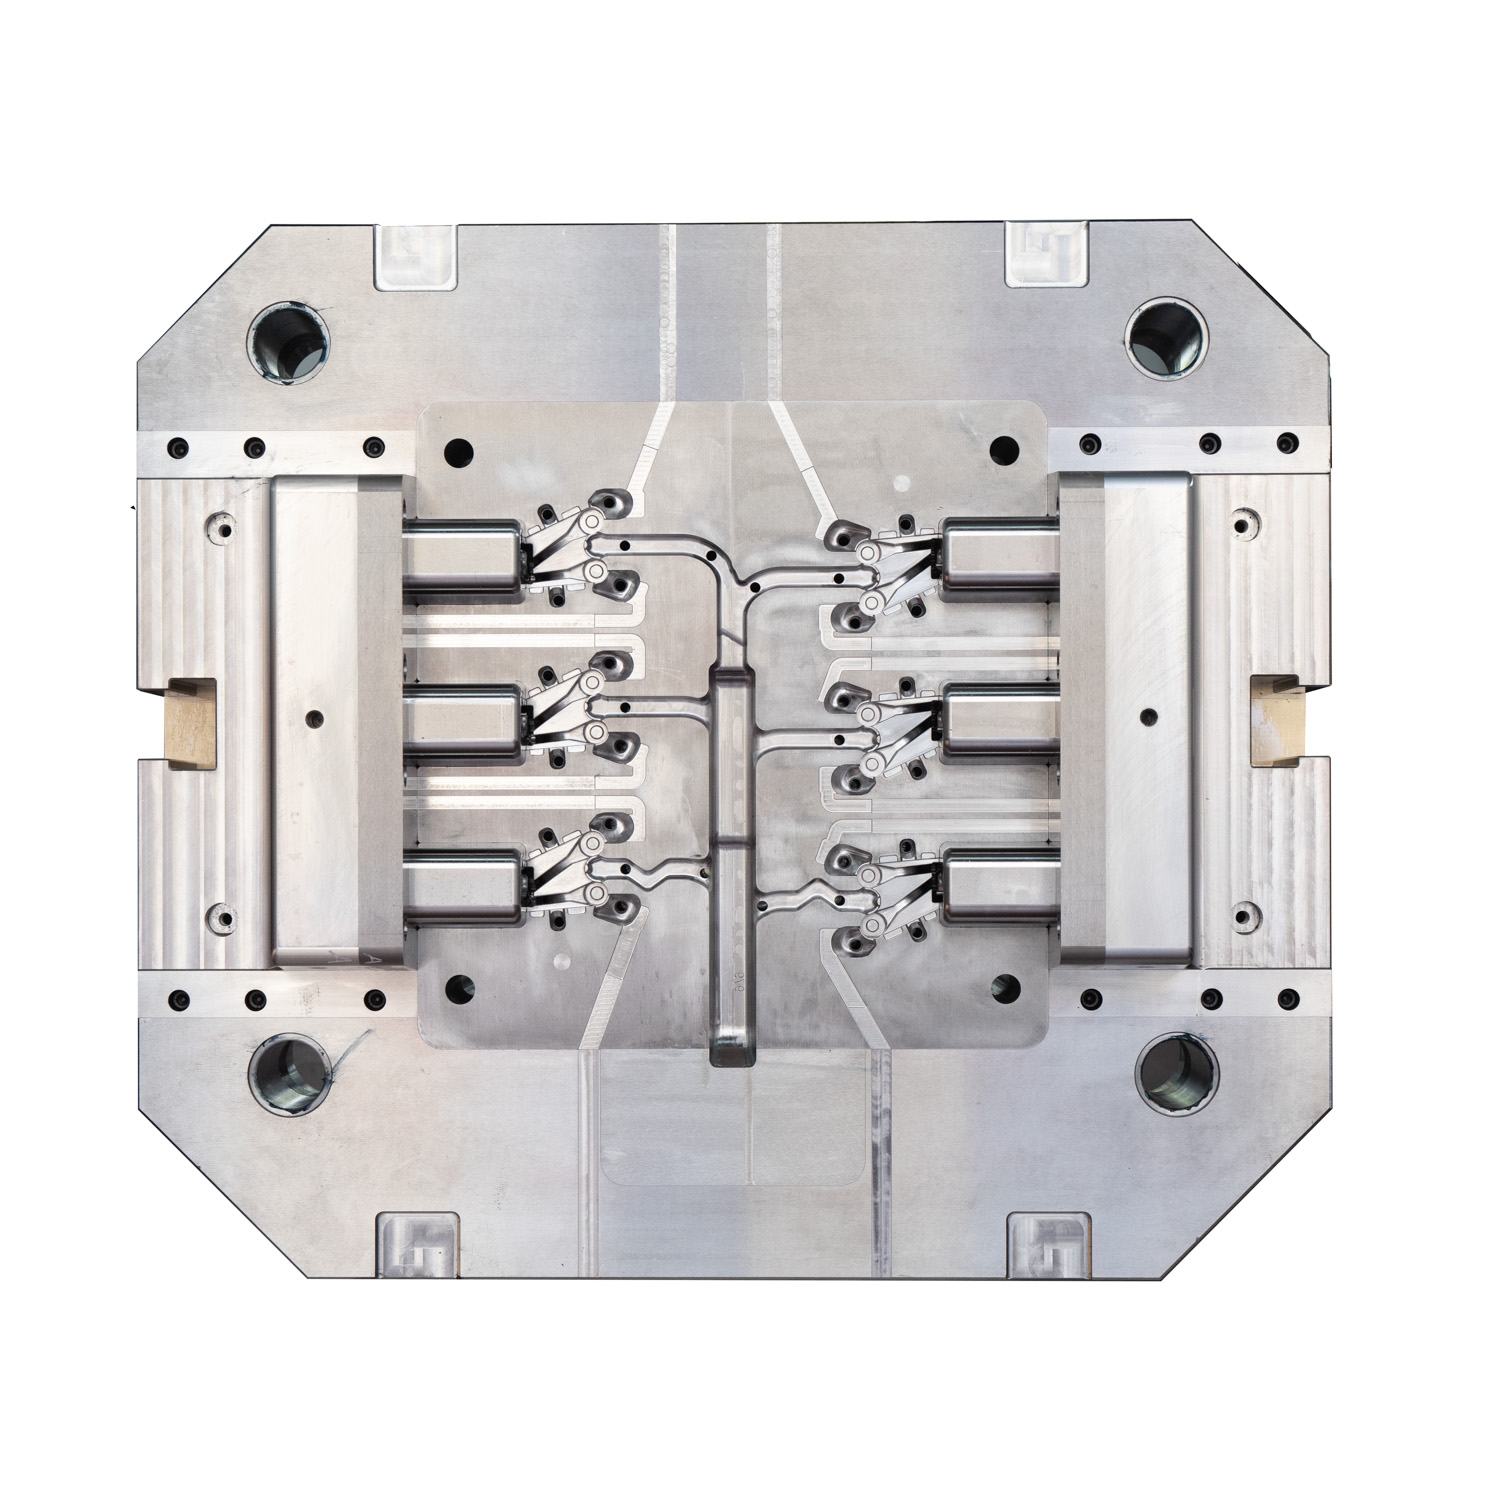
Representative tooling, machining and inspection work from our Kunshan facility.
FAQ
Questions, answered.
Which casting alloys do you tool for?
Aluminum ADC12/A380/A356, zinc Zamak 3 and 5, and magnesium AZ91D/AM60 are the most common. We select die steel and thermal design based on the alloy and wall thickness.
Can you reduce porosity in structural parts?
Yes. Vacuum-assisted filling, optimized overflows, jet cooling and die-temperature control are used together to minimize air entrapment and shrinkage porosity.
Do you build the trim die as well?
Yes. Trim dies, checking fixtures and secondary machining fixtures can be delivered with the die as a complete production package.
How do you validate a new die?
We run trial shots, inspect critical dimensions, check porosity where required, and document the process window before shipment. Samples are sent for your approval.
START A PROJECT
Have a mould project in mind?
Send us your part data and requirements. We will reply with a DFM review and a clear quotation within 24 hours.